Category: Fish feeding systems
Product guide · Feeding systemsAutomatic Fish Feeders — Types, Sizing & Supplier Quotes
Feed is 45–65% of operating cost, so the feeding system is the single piece of equipment with the clearest link to profitability. This guide covers the four main feeder types, how to size hoppers and delivery, what actually improves FCR, and what drives price.
Short answer: Automatic feeders range from timer feeders to acoustic shrimp feeders that listen to feeding activity and camera-assisted cage systems. Published trials show acoustic feeding works in shrimp ponds; feed or FCR savings for AI systems are mostly manufacturer claims, so ask for trial evidence.
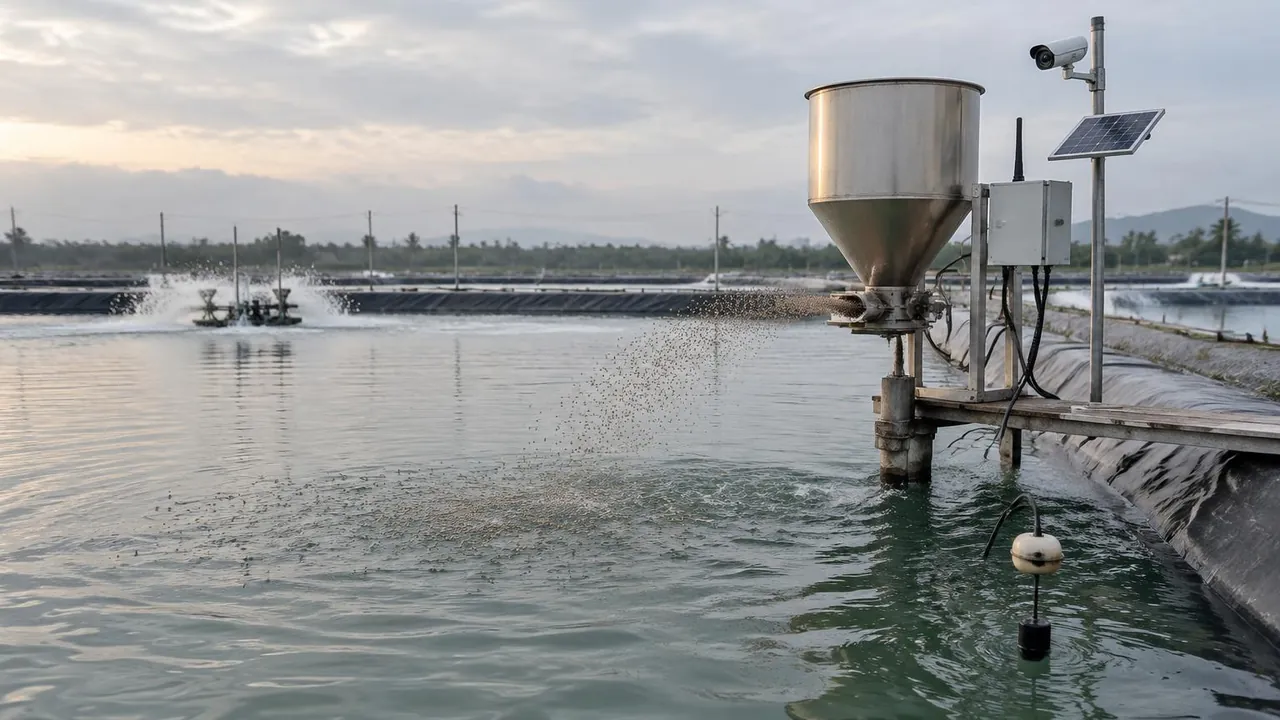
What automatic feeders do
- Timer feeders: hopper plus dosing mechanism on a schedule. Lowest cost, no feedback, best for stable low-intensity units.
- Demand feeders: fish trigger a pendulum or sensor to release feed. Very low cost per unit, strong FCR in trout and some finfish, unsuitable for shrimp.
- Acoustic / sensor-driven feeders: hydrophones or feed-waste sensors detect feeding activity and modulate dosing in real time. Standard in intensive shrimp, where they consistently cut FCR and shorten cycles.
- Centralised blower systems: silos plus rotary feeders and pneumatic pipework distributing feed to many tanks or cages from one control room. Standard in large RAS and salmon cage farms.
Where it applies
Technology maturity: Acoustic shrimp feeding: commercially established. Camera/AI feeding: commercial and emerging. Passive acoustic appetite research (2026): research.
Variants compared
| Variant | Best fit |
|---|---|
| Timer / scheduled feeders | Simple, low-cost; feed set amounts at set times regardless of appetite. |
| Acoustic shrimp feeders | Hydrophones detect shrimp feeding sounds and adjust feeding across many pond feeders; trade-body-reported trials since 2013. |
| Camera-assisted cage feeding | Video and sensor data guide feeding decisions; 2026 AI assistants give real-time recommendations to operators. |
| Central blower systems | Pneumatic distribution from a central silo to many cages or tanks. |
Typical specifications
| Parameter | Typical range | What it means for you |
|---|---|---|
| Hopper capacity | 20–500 kg (pond/tank units); 5–60 t silos | Size to 1.5–3 days of peak feed so refilling is not a daily bottleneck. |
| Feed pellet range | 0.5–12 mm | Confirm the mechanism handles both your smallest nursery crumb and largest grow-out pellet. |
| Dosing accuracy | ±3–8% per dose | Load cells or calibrated volumetric dosing; accuracy compounds across thousands of doses. |
| Throughput (centralised) | 300–2,000 kg/h per line | Sets how many tanks one line can serve within the feeding window. |
| Blow distance (pneumatic) | 50–400 m | Longer runs and more bends increase pellet breakage — specify pellet-friendly bends. |
| Power | 0.1–0.5 kW per unit feeder; 5–30 kW per blower line | Blower power dominates in centralised systems. |
| Control | Local timer, farm PLC or cloud app | Feeding records per tank per day are what auditors and lenders ask for. |
| Protection | IP65, UV-stabilised, marine-grade for cages | Feed is hygroscopic — moisture ingress causes bridging and blockages. |
Advantages
- Feeds more often in smaller meals
- Demand-based systems react to appetite
- Records feed data per pond or cage
Limitations
- AI feed-saving claims rarely independently tested
- Needs reliable power and connectivity
- Sensors and hydrophones need cleaning
Maintenance
- Clean hoppers and dispensers to avoid caking
- Check hydrophones/cameras for fouling
- Calibrate feed-rate output against weighed feed
Risks to manage
- Overfeeding raises oxygen demand and degrades water quality — combine feeding with DO monitoring
- Feed reduction claims vary by farm; treat FCR improvements as unverified until tested on your site
Compliance points to check
- Electrical safety and outdoor ratings for pond equipment
- Feed records support certification and traceability audits
Compliance points are prompts for your own review. Producers, suppliers and buyers remain responsible for the rules that apply to them; FishMatch does not certify equipment or guarantee compliance.
Sizing guidance
Size the feeding system on peak daily feed at end of cycle and the feeding window you want, then check the hopper refill interval and the number of tanks or ponds each line must serve.
| Project scale | Indicative feeding system | Design notes |
|---|---|---|
| Nursery / hatchery tanks | Belt or micro-dosing feeders | Frequent small doses matter more than capacity; ensure crumb sizes do not bridge. |
| Pond shrimp, up to 5 ha | Timer or acoustic feeders, 1–2 per ha | Acoustic units typically pay back within 1–2 cycles through FCR and cycle length. |
| Tank grow-out / small RAS | Per-tank hopper feeders on farm PLC | Per-tank feed logging is required for reliable biomass and FCR tracking. |
| Large RAS or cage farm | Centralised silo + blower distribution | Design line capacity around peak-day feed within the feeding window, plus a spare line. |
Peak daily feed ≈ standing biomass × feeding rate (%/day). Typical feeding rates run 1.5–3% for grow-out finfish and 2–4% for shrimp at mid-cycle, falling as fish grow. Size the hopper for 1.5–3 days of that figure and the delivery line for peak day within your feeding window.
How to choose
- Feedback beats schedule
In intensive shrimp, acoustic feeders typically reduce FCR by 5–15% versus fixed schedules. On feed at 50–65% of OPEX, that is the fastest payback on the farm.
- Pellet integrity
Aggressive augers and sharp pneumatic bends create fines that fish will not eat and that pollute the water. Ask for breakage test data.
- Per-tank records
Feed logged per tank per day underpins FCR, biomass estimates and lender reporting. Confirm export and API access, not just an app view.
- Moisture and bridging
Sealed hoppers, vibration or agitation, and a documented cleaning routine — bridging is the most common operational complaint.
- Redundancy
A failed centralised line stops feeding on many tanks at once. Specify a spare line, manual bypass or portable feeders.
- Service and spares
Motors, augers, dosing discs and sensors are wear parts. Confirm regional support and spares lead times before ordering.
What drives the price
- Feeder type
Timer < demand < acoustic < centralised pneumatic, by roughly an order of magnitude across the range.
- Sensing and control
Hydrophones, load cells, cameras and cloud analytics are the main cost step above basic dosing.
- Hopper / silo capacity
Silos, structure, foundations and filling equipment can exceed the feeders themselves.
- Distribution pipework
In centralised systems, pipe runs, selectors and bends often outweigh the blower cost.
- Environment rating
Marine cage duty and tropical UV exposure add cost over sheltered tank installations.
- Integration
PLC/SCADA integration and data export are engineering scope, not a checkbox.
Sourced example: a University of Minnesota RAS study (2024 figures) used USD 1,000 per tank feeder, a figure its survey respondents agreed was reasonable; the feeder type is not specified and some cost less. Acoustic pond feeders and centralised silo-and-blower systems: not sourced.
Common specification mistakes
- Buying fixed-schedule feeders for intensive shrimp and paying the FCR penalty every cycle.
- Undersizing hoppers so staff spend the working day refilling instead of observing stock.
- Ignoring pellet breakage in long pneumatic runs, then blaming water quality on the biofilter.
- No per-tank feed data, which makes FCR, biomass and lender reporting guesswork.
- No redundancy on a centralised line, so one blower failure stops feeding farm-wide.
Quote checklist for automatic feeders
State these in your request so offers are priced on the same basis. If you do not know a value yet, write “unknown” — suppliers must then state the assumption they used, and our team flags differences when comparing.
- Hopper capacity — your required value, or “unknown”
- Feed pellet range — your required value, or “unknown”
- Dosing accuracy — your required value, or “unknown”
- Throughput (centralised) — your required value, or “unknown”
- Blow distance (pneumatic) — your required value, or “unknown”
- Power — your required value, or “unknown”
- What it serves — species or product, life stage or grade, and the capacity it must handle (peak load, not annual average)
- Site and climate — country, water source, temperature and salinity range or ambient conditions, power supply
- Quantity, destination and timing — number of units, delivery point and terms, required delivery and commissioning dates
- Documents you need — manuals, test or performance reports and any conformity or electrical certificates required where it will be installed; no certification is assumed
Capacity, operating conditions, materials, quantity, delivery terms and installation scope change the price most — see what drives the price above. Send this checklist as a reviewed project request.
Components that work with it
- Water quality sensors
DO feedback prevents feeding when oxygen is low
- Paddlewheel aerators
Aeration must match the feed load
Plan before you request quotes
Free calculators give a first sizing or cost scenario from your own inputs. Results are estimates to discuss with suppliers, not quotations.
Automatic feeders — buyer questions
Get quotes for automatic feeders
Send your duty, site conditions and target capacity once. We turn it into a comparable specification, send a confidential RFQ to producers and suppliers that may fit the project, and coordinate their replies on the same scope. Free for buyers; qualifying projects start at USD 250,000. FishMatch does not manufacture equipment, and buyers do not contact suppliers directly.
Related pages
Sources and review
- Acoustic feedback improves automated feeding systems for shrimp — Global Seafood Alliance, 2020-04
- Shrimp bioacoustics: feeding behavior and precision aquaculture — Global Seafood Alliance, 2026-09
- RACE Autofôring research project (2025–2027) — SINTEF
- An Economic Feasibility Analysis of Food Fish Aquaculture in Minnesota (Tables 16 and 23; figures from 2024 expert interviews) — University of Minnesota, 2025-06
Ranges marked "manufacturer-stated" come from public manufacturer documentation reviewed by FishMatch; they are examples, not guarantees, and supplier names are not shown. Last reviewed 2026-10-24.